
Capabilities
From bench to market, on one platform.
Plug in at any stage. Engage a single service — or hand us the full lifecycle, from first formulation to the customer’s door.
01 · Research & development
Develop with the team that will make it.
Dedicated R&D and QC lab space, staffed by scientists who have taken regulated products from concept to commercial release. Because development sits next to production, scale-up and technology transfer happen in the same building.
- Formulation and process development
- Feasibility studies and pilot batches
- Analytical and QC method support
- Technology transfer into production
02 · Production
Controlled-environment manufacturing.
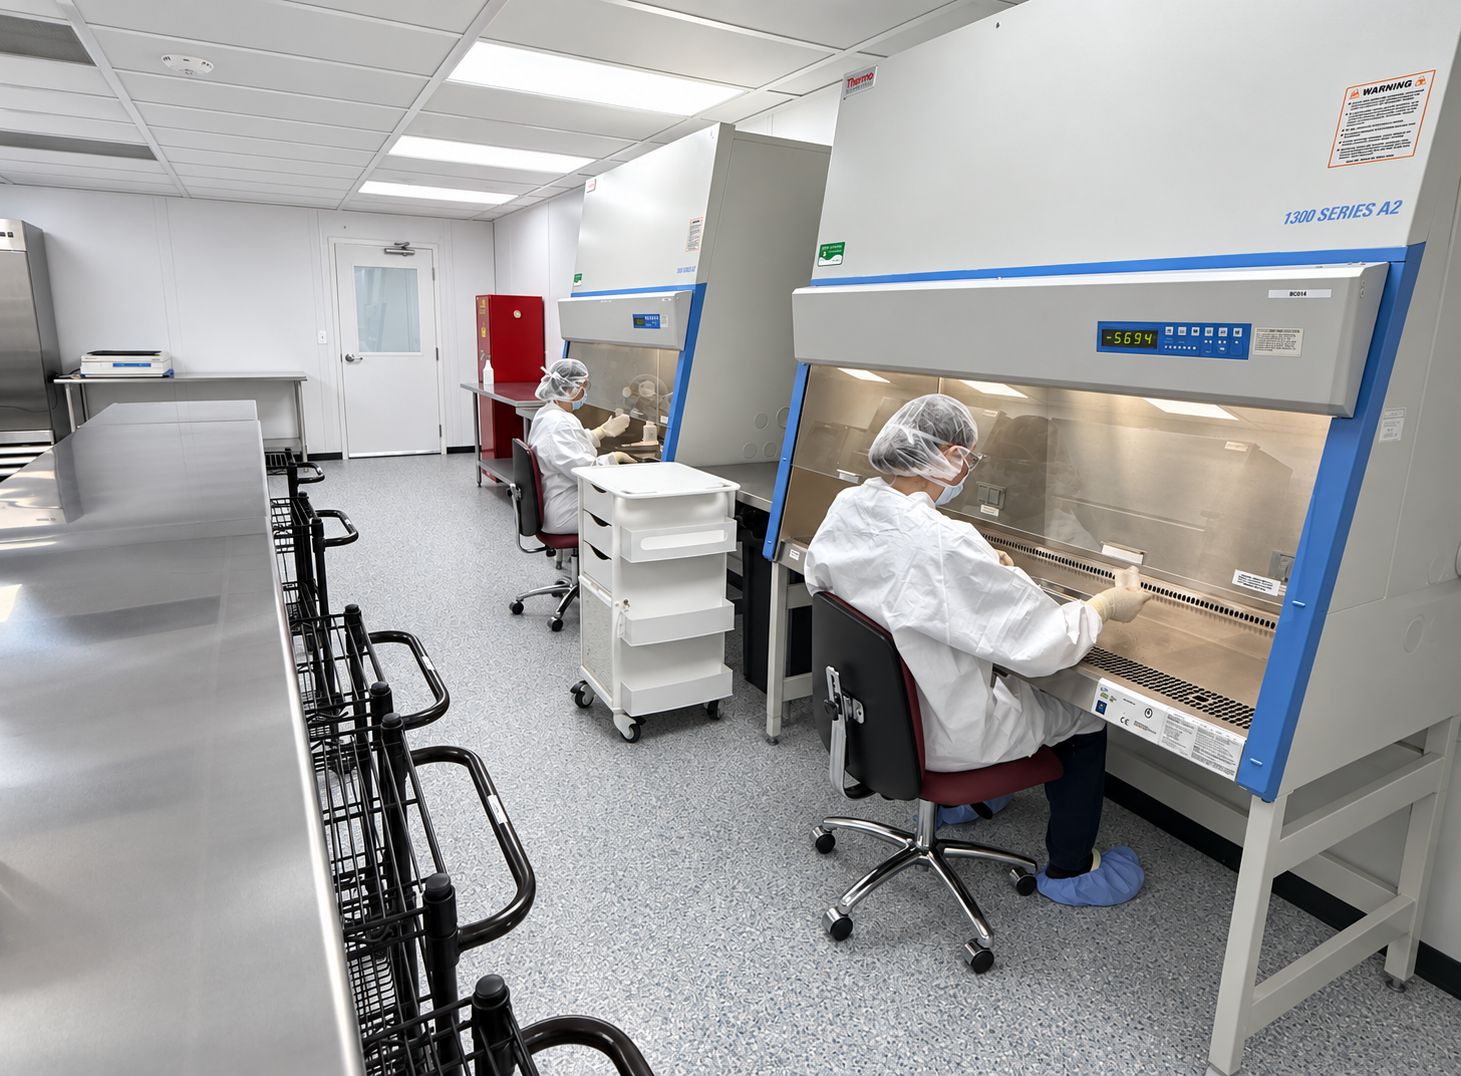
Production runs in 2,600 ft² of ISO 7 / ISO 8 cleanroom space, with ISO 5 biosafety cabinets for aseptic work — the same environment we use for human tissue-based products.
- Aseptic processing under ISO 5
- Material preparation and controlled processing
- Packaging in controlled environments
- Pilot through commercial-scale runs, scoped to your product
03 · Lyophilization
Freeze-drying, in-house.
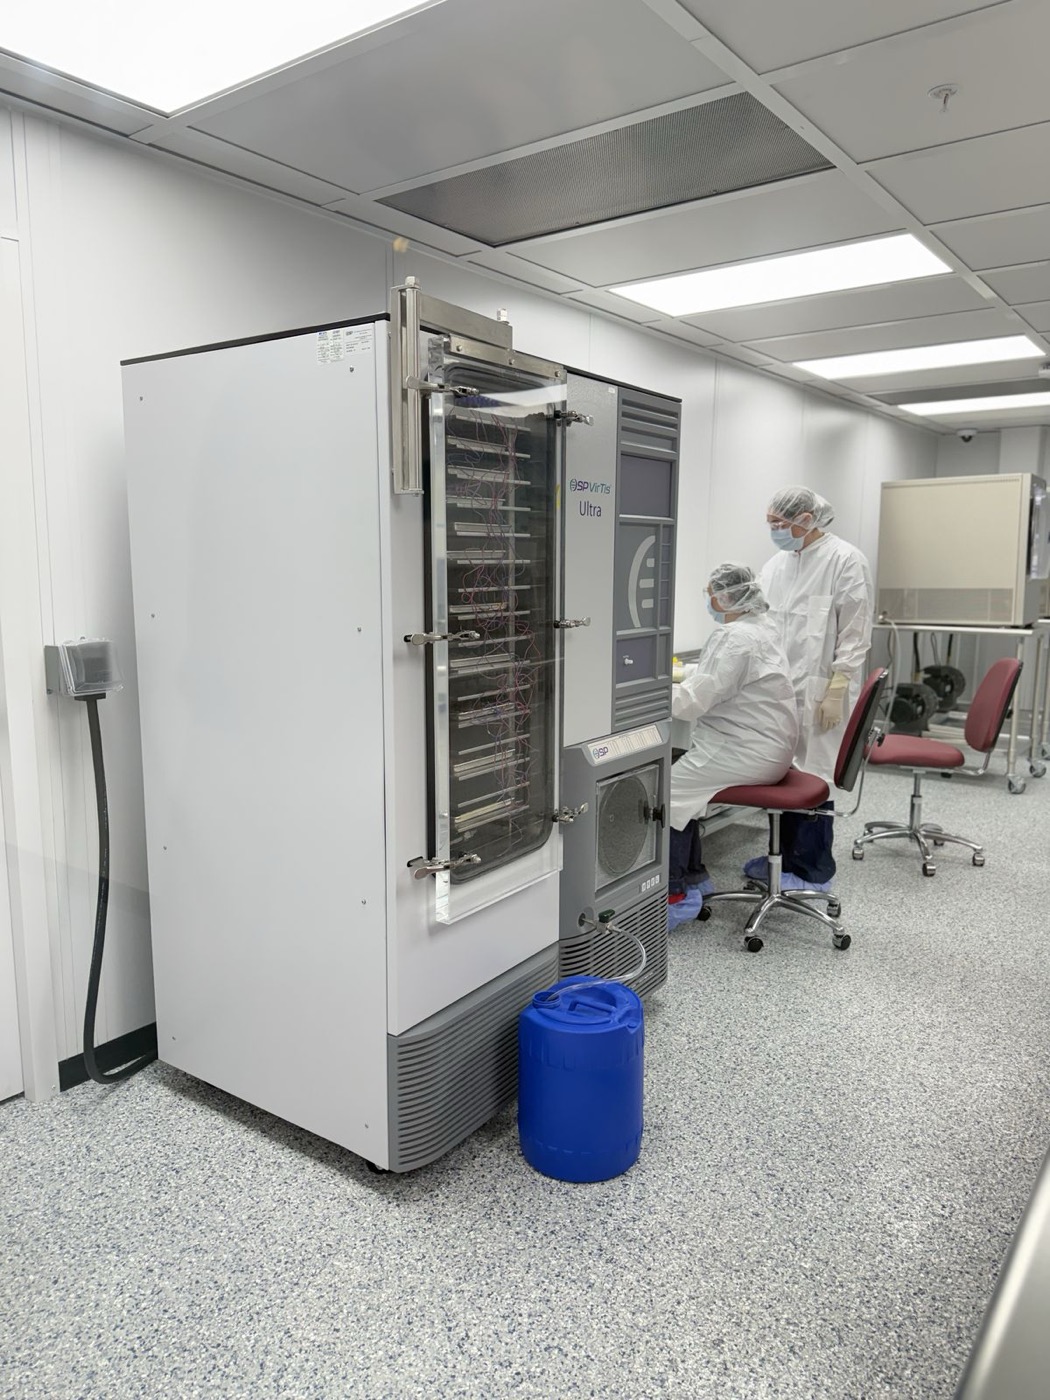
A production-scale lyophilizer inside the cleanroom suite removes water while preserving product structure — improving stability and shelf life for biologics, peptides and other moisture-sensitive products.
- Cycle development support for new products
- Production-scale freeze-drying
- Integrated with aseptic processing and QC
- Available as a standalone, subcontracted step
04 · Quality & regulatory
A quality system you operate inside — not one you have to build.
Partner programs run within our quality management framework, aligned with ISO 13485, and processes designed to meet applicable FDA requirements — including 21 CFR Part 1271 for human cells, tissues and cellular and tissue-based products.
- Document control and batch records
- Continuous environmental monitoring
- QC testing and release support
- Quality agreements for every partner program
- Regulatory pathway guidance from a team that has done it
ISO 13485
Quality management system aligned with ISO 13485, the medical-device quality standard.
ISO 7 / ISO 8
Classified modular cleanrooms with controlled material and personnel flow.
ISO 5
Biosafety cabinets for aseptic, open-product processing.
21 CFR 1271
Processes designed to meet applicable FDA requirements for HCT/Ps.
05 · Commercialization
The commercial engine behind our own products — available to yours.
Most manufacturing partners stop at the loading dock. We take our own products to market every day, and partners can use the same teams and channels.
Go-to-market strategy
Positioning, launch planning and channel strategy for the U.S. market.
Sales & distribution
Access to our sales organization and authorized distribution partners.
Reimbursement & market access
Support from teams who navigate reimbursement for our own products.
Customer & clinical support
Customer service and clinical-support functions for your customers.
Tell us what you’re building.
We’ll respond to schedule a confidential discovery call — or an in-person or virtual tour of the Salt Lake City facility.